Featured Wheel Service Parts & Equipment
Explore our factory-direct catalog of CE-certified tubeless valves, precision balancing machinery, TPMS repair components, and lead-free wheel weights engineered for international export.
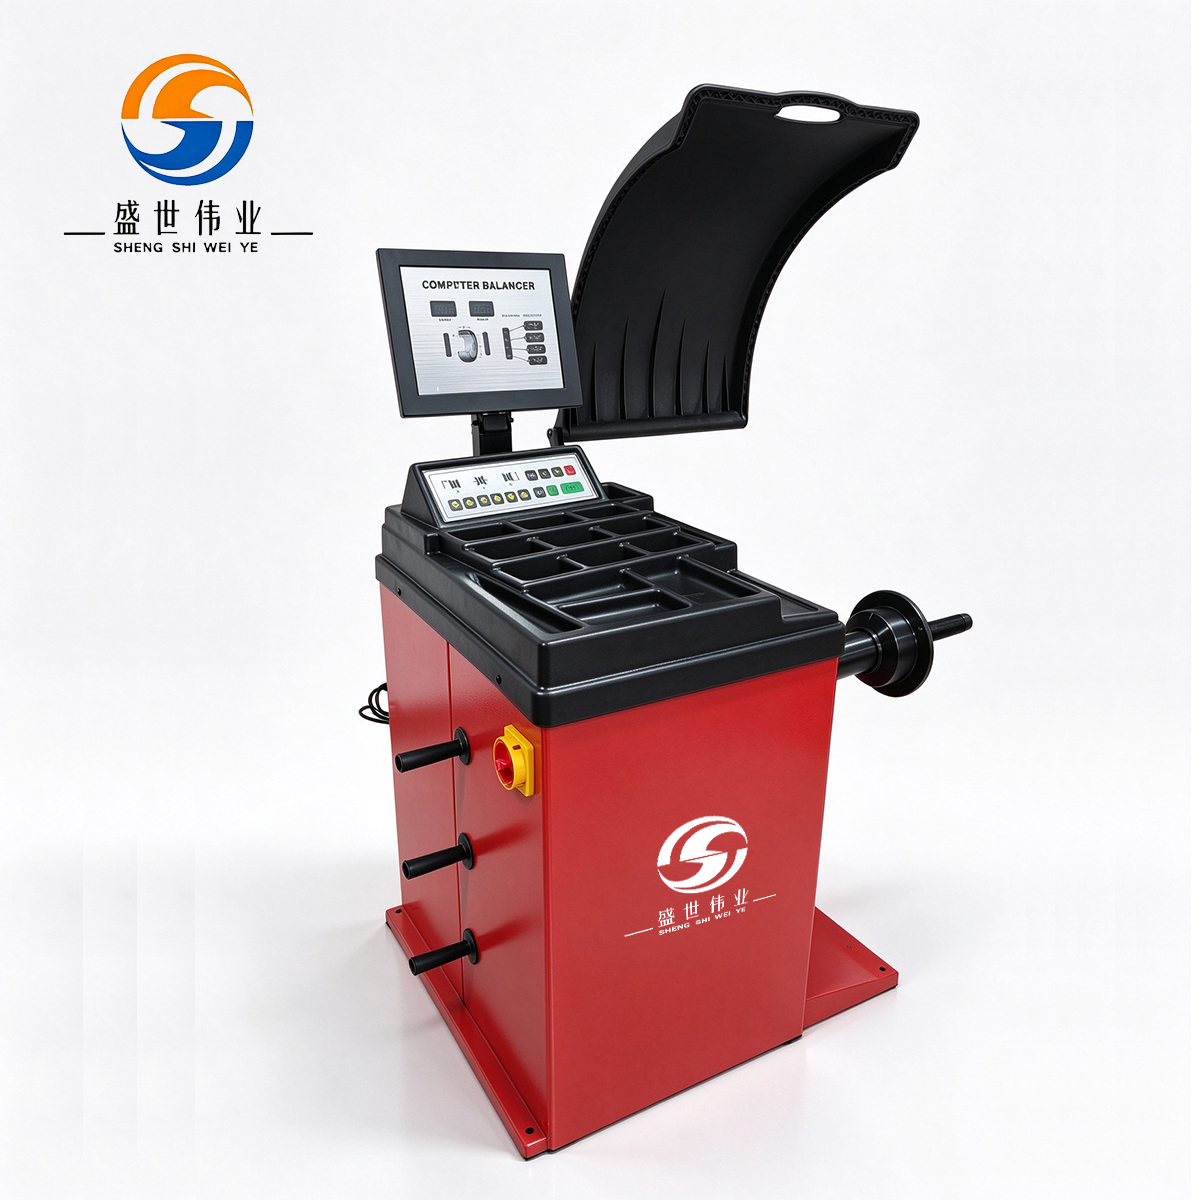
Fully Automatic High Precision Tire Balancer Wheel Balancing Machine for Car Repair Shop
View Specs
Tpms Sensor Valve Stem Repair Kit Auto Parts Pressure Sensor Tyre Valve
View Specs
Universal PVR70 Bent Valve Stems for Tubeless Tires
View Specs
TPMS-17 High Strength Aluminum TPMS Valve Stem Replacement Universal Snap-in Component
View Specs
Fe Stick on Wheel Weights Auto Parts Round Corner Balance Block
View Specs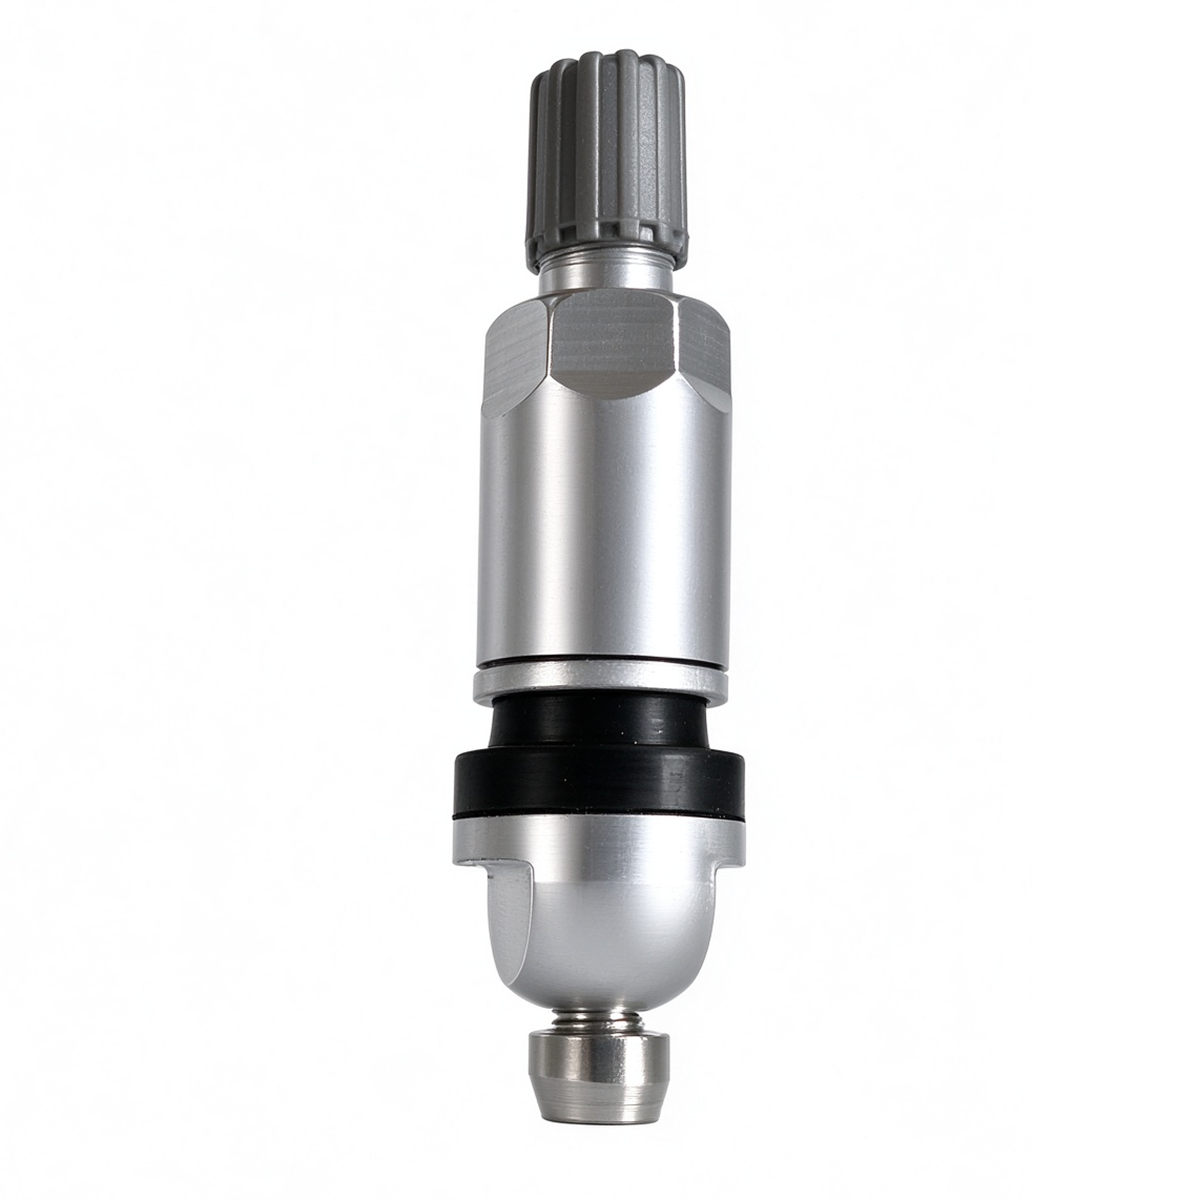
Aluminum Alloy Valve TPMS Tire Pressure Monitoring Device Tire Inflation Valve
View Specs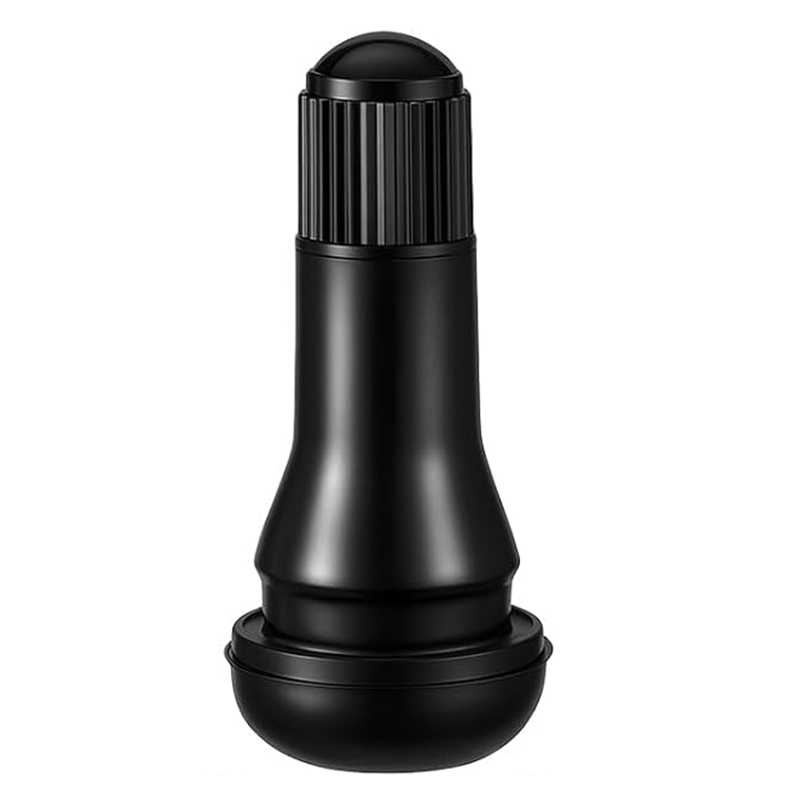
Factory Direct Tire Valve Easy Installation Tubeless Rubber Snap-In Valve
View Specs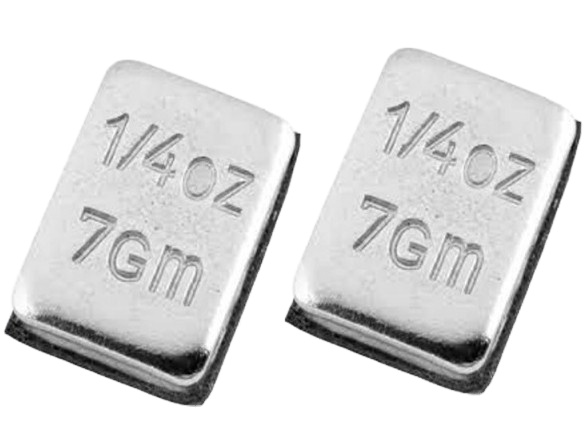
World Standard 1/4 OZ Zinc Plated Stick-On Tape Adhesive Tire Wheel Balancing Weight Strip
View SpecsTR48E Motorcycle Clamp-In Valve Metallurgical & Mechanical Analysis
The TR48E motorcycle tire valve represents the industry benchmark for high-speed, high-pressure tubeless rim configurations. Unlike standard rubber snap-in valves (such as TR412 or TR413) that suffer from elastomeric flexing and degradation under extreme rotational centrifugal forces, the TR48E features a rigid metal clamp-in architecture. Manufactured from high-tensile brass alloy (CuZn39Pb2) or anodized lightweight aluminum, the TR48E stem maintains structural integrity at speeds exceeding 250 km/h, preventing centrifugal air loss and rim seat deflection.
In modern two-wheeler engineering, particularly across the demanding transit corridors of Dnipropetrovsk Oblast, tire pressure consistency directly correlates with rider safety, handling precision, and tread longevity. The TR48E utilizes a 90-degree or 45-degree angled design options (and short straight profiles) specifically engineered to fit tightly recessed motorcycle wheel rims where brake discs, sprocket assemblies, and hub castings restrict air chuck clearance during maintenance.
| Parameter | TR48E Standard Specification | Testing Standard / Compliance | B2B Sourcing Advantage |
|---|---|---|---|
| Stem Material | High-Grade Brass (CuZn39Pb2) / Anodized Aluminum | EN 12164 / ASTM B16 | Zero structural flexing under high centrifugal shear force |
| Rubber Grommet Compound | EPDM / High-Density Fluororubber (FKM) | ISO 4892-2 (Ozone & UV Aging) | Cold-resistant to -40°C; resistant to road salt & oil |
| Maximum Cold Inflation Pressure | 14 Bar (200 PSI) Operating Rating | SAE J1205 / DIN 7756 | Accommodates high-pressure sport & heavy touring tires |
| Rim Hole Compatibility | 8.3mm (0.327") or 11.5mm (0.453") Standard Fit | ETRTO V2.03.1 Standard | Universal fitment across OEM & aftermarket alloy wheels |
| Valve Core Insertion Torque | 0.25 N·m - 0.35 N·m (2.2 - 3.1 in-lbs) | ISO 10231 Testing Protocol | Pre-installed leak-tested internal brass core with PTFE seal |
| Tightening Nut Torque Rating | 3.5 N·m - 4.5 N·m (31 - 40 in-lbs) | Factory Automated Calibrated Seating | Double-nut or locking washer system prevents vibration loosening |
| Surface Corrosion Protection | Nickel-Plated / Chrome / Anodized Surface Coating | ISO 9227 Salt Spray Test > 480 Hours | Impervious to winter road de-icing chemicals in Eastern Europe |
Structural Durability vs. Centrifugal Deflection
When a motorcycle tire rotates at 100 km/h, a standard rubber snap-in valve experiences continuous bending moment forces. Over time, micro-cracks form around the rubber stem base, causing gradual pressure drops. The TR48E clamp-in construction locks directly onto the rim valve hole with dual elastomeric EPDM washers and a threaded locknut. This creates a mechanical seal that remains entirely immune to dynamic wobble, tire vibration, and shock impacts from uneven road surfaces.
Localized Application Scenarios in Dnipro & Dnipropetrovsk Oblast
Understanding regional road conditions, seasonal temperature fluctuations, and commercial fleet requirements is critical for automotive parts importers in Ukraine's central industrial hub.
Sub-Zero Winter Weather & Chemical Endurance
Dnipro experiences harsh continental winter cycles with temperatures plunging below -20°C, accompanied by heavy application of calcium chloride and road salt along major arteries such as Slobozhanskyi Avenue and the Central Bridge. Standard rubber valves harden and crack under freezing thermal stress. Cangzhou Olsik’s TR48E valves utilize specialized low-temperature EPDM grommets rated to -40°C combined with nickel-plated solid brass stems that completely prevent corrosion and air seepage during winter operation.
Urban Express Delivery Fleets & Commercial Motos
The rapid expansion of courier, postal, and last-mile delivery services across Dnipro city center (from Shevchenkivskyi district to Industrialnyi) has placed unprecedented mileage demands on light commercial 2-wheeler fleets. Daily stop-and-go driving over tram tracks and cobblestone routes subjects tires to heavy vibration. TR48E clamp-in valves eliminate frequent valve stem failure, reducing downtime for commercial fleet operators and auto service networks (СТО).
Intercity Highway Transit (Route M04 & M18)
High-speed long-distance riding along regional highways connecting Dnipro to Zaporizhzhia and Kryvyi Rih demands maximum pressure holding capacity. At sustained speeds of 120-180 km/h, tire temperatures rise rapidly while centrifugal force pulls straight rubber stems outwards. The TR48E's secure mechanical clamping collar guarantees that the valve angle remains fixed, shielding internal cores from heat build-up and pressure spikes.
Dnipro Automotive Aftermarket Sourcing Trends & Compliance Standards
As Ukraine aligns its transport and safety regulations with European Union standards, local automotive accessory importers and distributors in Dnipro face evolving compliance requirements and supply chain shifts.
Mandatory CE & ISO Compliance
Importers across Dnipropetrovsk Oblast increasingly require CE certification, ISO 9001 quality management verification, and TÜV performance compliance to ensure imported wheel parts pass strict domestic transport safety audits.
Multimodal Western Corridor Logistics
Direct ocean shipments to Odesa are supplemented by rail and truck transit through Polish (Gdańsk/Gdynia) and Romanian (Constanța) ports. Our export packaging features reinforced 5-ply corrugated cartons and palletized shrink-wrap to withstand multi-stage transit to Dnipro warehouses.
Private Label & Custom OEM Packaging
To differentiate in a competitive wholesale market, Dnipro distributors leverage our custom OEM branding services—including customized blister pack cards, inner box prints, and custom laser-etched logos on TR48E valve stems.
Engineering Comparison: TR48E Clamp-In vs. Traditional Rubber Valves
A comprehensive technical audit demonstrating why professional repair stations (СТО) in Dnipro are upgrading from snap-in rubber stems to rigid metal clamp-in solutions.
| Evaluation Feature | Cangzhou Olsik TR48E Brass Clamp-In | Standard TR412 / TR413 Rubber Snap-In | Generic Low-Cost Aluminum Valves |
|---|---|---|---|
| Mechanical Mounting Integrity | Superior Threaded collar + Dual EPDM gaskets | Friction fit snap-in rubber groove | Single nut clamp-in without lock washer |
| Pressure Resistance Limit | Up to 14 Bar (200 PSI) burst safety margin | Max 4.5 Bar (65 PSI) recommended | Typically 7 - 9 Bar (100 PSI) |
| High-Speed Stability (>150 km/h) | Zero deflection; zero rim separation | Subject to flexing and centrifugal air weeping | Moderate stiffness; risk of thread stripping |
| Service Lifespan | 5+ Years (outlasts multiple tire changes) | Must be replaced at every tire change (1-2 yrs) | 2-3 Years (aluminum thread galling risk) |
| Extreme Cold (-20°C to -40°C) | EPDM retains elasticity; stem remains rigid | Rubber becomes brittle; prone to base cracking | Seals harden if using low-grade SBR rubber |
| Corrosion Resistance | Nickel/Chrome Plated over CuZn39Pb2 Solid Brass | Brass insert coated in vulcanized rubber | Raw anodized aluminum subject to galvanic corrosion |
Factory Manufacturing Capabilities & Quality Control Protocol
Cangzhou Olsik Automobile Accessory Co., Ltd. (established 2006) operates a 10,000+ m² modernized facility dedicated to tire servicing supplies and workshop equipment.
1. Precision Machining & Automated CNC Stamping
Our TR48E valve bodies are machined on multi-axis automated CNC lathes to achieve exact thread pitch dimensions matching ETRTO V2.03.1 standards. This guarantees effortless installation with standard air inflation chucks and pressure monitoring sensors.
2. 100% Automated Pneumatic Leak Testing
Every single batch of TR48E valves undergoes 100% pressure-hold testing prior to packaging. Valves are pressurized with dry nitrogen to 1.0 MPa (145 PSI) underwater or in automated helium detection chambers to detect micro-porosity defects.
3. Comprehensive Certification & Compliance
Cangzhou Olsik holds certified ISO 9001:2015 Quality Management qualifications along with CE, GS, and TÜV product marks. Full Material Test Reports (MTR) and Certificates of Conformance (COC) are supplied with every wholesale export order to Dnipro.
Professional Installation Protocol for TR48E Valves in Workshop Service Stations
Following standard operating procedures ensures leak-free performance and maximizes safety for two-wheeler service centers in Dnipro.
Rim Valve Hole Preparation
De-burr the alloy rim valve hole (8.3mm or 11.5mm) using a fine deburring tool. Clean away metal shavings, residual rubber, or old corrosion with solvent to ensure a smooth, clean sealing surface.
Grommet Seating & Stem Insertion
Fit the inner EPDM rubber grommet onto the base of the TR48E brass stem. Insert the stem from the interior of the wheel rim outward, ensuring the grommet seats squarely against the inner rim drop-center profile.
Outer Washer & Locknut Torquing
Place the outer metal washer and exterior EPDM gasket over the protruding stem thread. Thread the brass locknut by hand, then tighten with a calibrated torque wrench to exactly 3.5 N·m - 4.5 N·m. Do not over-torque.
Pressure Testing & Core Inspection
Mount the tubeless tire, inflate to operational pressure (2.5 - 3.5 Bar), and inspect the valve base and core with bubble leak detection spray. Verify valve core torque at 0.25 - 0.35 N·m before attaching dust cap.
Frequently Asked Questions for Dnipro Importers & Wholesalers
Answers to common commercial, logistical, and technical questions asked by purchasing directors and automotive accessory importers in Ukraine.
What certifications do Cangzhou Olsik TR48E tire valves hold for import into Ukraine? +
What is the Minimum Order Quantity (MOQ) for TR48E valves and combined shipments? +
How do you ship wholesale automotive orders to Dnipro, Ukraine under current conditions? +
Are TR48E valves resistant to freezing winter temperatures and road salt in Dnipropetrovsk Oblast? +
Can we request customized laser engraving or private-label packaging for our Dnipro retail chain? +
What are the accepted payment methods and trade terms for B2B contracts? +
What warranty or quality assurance guarantee is provided with Olsik products? +
How quickly can we receive production samples for technical testing in Dnipro? +
Partner with a Trusted CE Certified Valve Manufacturer
Direct factory pricing, strict quality control, and dependable supply chains tailored for automotive distributors, wheel rim manufacturers, and tire service networks across Dnipro and Eastern Europe.
Contact Us